Industrial Reverse Osmosis (RO) Systems: Unlocking Efficiency and Quality


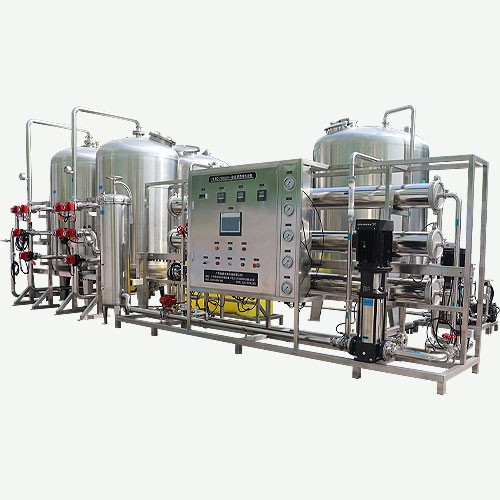


Industrial reverse osmosis systems give factories, utilities, and process plants a reliable way to turn difficult feed water into clean, consistent, high-purity water. At their core, these systems push pressurized water through a semi-permeable membrane that removes up to 99.9% of dissolved salts, along with bacteria, particles, organics, and heavy metals. As a result, one well-engineered system can serve drinking water, boiler feed, bottling, and ultrapure applications from a single skid.
Chunke designs and manufactures industrial reverse osmosis systems for export markets across the Middle East, Africa, Southeast Asia, the CIS, and South America. Moreover, we build every system around your actual feed water and daily demand rather than a one-size-fits-all catalogue unit. Because of that engineering-first approach, our machines deliver stable output, low downtime, and a long membrane life even in tough conditions. In the sections below, you will find how the technology works, real capacity ranges, the components that separate a professional system from a cheap one, and the criteria that help you choose correctly.
Hence, CHUNKE produces a wide range of designed and custom industrial reverse osmosis systems. So it is ranging in capacity from 2000 to 180.000.000LPH to meet every industrial water treatment need and application. So, these energy efficient industrial RO equipment produces high-quality water at an affordable economic cost.
Furthermore, our industrial ro systems are delivering high quality water under the most difficult requirements of ongoing operation and corrosive conditions. Also we design them with selectable functional, control features and additional apparatus supplying user’s the capacity to custom-make your reverse osmosis machine. Whatever your water treatment application requires, our industrial reverse osmosis system will be your optimal solution.
What Is an Industrial Reverse Osmosis System?
An industrial reverse osmosis system is a large-scale water purification plant that forces feed water through spiral-wound membranes under high pressure. Consequently, dissolved ions and contaminants stay behind in a concentrate stream while purified water — called permeate — passes through. Unlike a small domestic unit, an industrial system runs continuously, handles high flow rates, and integrates pre-treatment, energy-efficient pumping, instrumentation, and automated controls.
These systems differ from commercial or household RO in scale and robustness. For example, a home unit produces a few hundred litres per day, whereas an industrial reverse osmosis machine can produce anywhere from 2,000 litres per hour to 7,500 cubic metres per day. In addition, industrial platforms use industrial-grade pumps, stainless steel or FRP frames, and PLC control so operators can run the plant safely around the clock. You can explore our full commercial and industrial reverse osmosis systems range to see how each platform is configured.
Because water quality standards vary by industry, an industrial system is rarely a single box. Instead, it is a treatment train that matches the feed source, the target purity, and the plant’s uptime requirements. Therefore, the right design starts with a water analysis, not a price list.
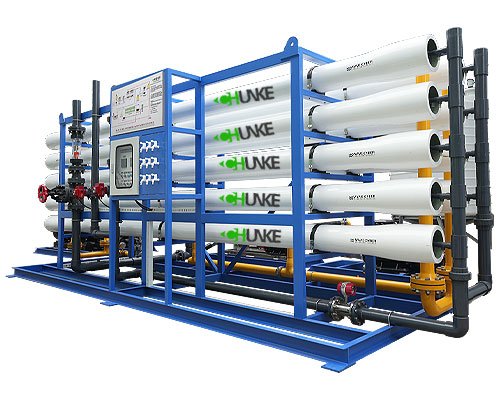
Compact industrial inverse osmosis plant:
In addition, CK-RO Series industrial tap water reverse osmosis water treatment equipment is equipped with media filters. And chemical dosing systems (pre chlorination, antiscalant, dechlorination, post chlorination and post pH). So, this equipment is primarily customized to suit individual customers and different water applications. CK-RO Series is one of the most compact industrial reverse osmosis system on the market, built with energy saving 8040 ro membranes. accordingly
The design of the CK-RO Series skid mounted industrial reverse osmosis system, takes into consideration certain water problem. Along with it is robust construction, user friendly design, environmentally friendly material, economic, easy operating and long-term reliability.
Also you can choose your ro system as containerized reverse osmosis water treatment plant.
The process of industrial reverse osmosis machine:
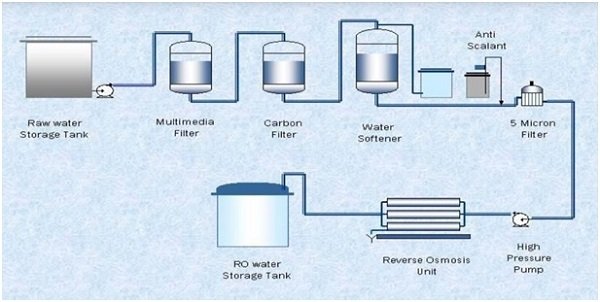
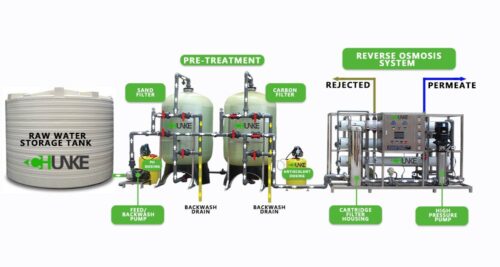
Industrial reverse osmosis plant includes a multimedia pretreatment tanks, water softener, antiscalant dosing system. And also it has antifouling dosing system, reverse osmosis unit with semi-permeable inverse osmosis membranes, ozone generator and ultraviolet sterilizers or post chlorination as a post treatment. These RO machines apply the new technology of reverse osmosis by sending feed water through a multimedia prefilter to remove particles that are larger than 10 micron. Then the water goesvia an antiscalant chemical to control hardness fouling that may cause damage to the membranes of the RO machine.
So, these pretreatment options have the capability of removing hardness, chlorine, odors, color, iron, and sulfur. The water then continues into the reverse osmosis unit where a high-pressure pump applies extreme pressure to the highly concentrated solution, separating the remaining salts, minerals, and impurities that the prefilter cannot catch. In addtion, fresh, potable water comes out from the low pressure end of the membrane while salts, minerals, and other impurities are discharged into a drain on the other end. Lastly, the water is passed through a UV sterilizer (or post chlorination) to kill any bacteria and microbes that still exist in the water.
How an Industrial Reverse Osmosis System Works
Every industrial reverse osmosis system follows the same logical sequence, yet the engineering behind each stage decides how well the plant performs over years of service. First the water is conditioned, then it is pressurized through the membranes, and finally it is polished to the exact quality your process needs. Below, we break down each stage so you can see what matters.
1. Pre-Treatment: Protecting the Membranes
Pre-treatment removes the suspended solids, hardness, chlorine, and fouling agents that would otherwise destroy the membranes. Typically, this stage combines multimedia filters, activated carbon, antiscalant dosing, and a 5-micron cartridge filter. As a result, the Silt Density Index (SDI) drops to a safe level below 3–5 before water ever reaches the RO array. For challenging surface water, we often add ultrafiltration pre-treatment to guarantee stable membrane feed.
2. High-Pressure Pumping and the Membrane Array
Next, a high-pressure pump drives the conditioned water into pressure vessels holding spiral-wound membranes. For brackish water, operating pressure usually sits between 10 and 25 bar, while seawater demands 55 to 80 bar. Because the pump is the heart of the system, Chunke specifies reliable units from proven makers such as Grundfos and Danfoss high-pressure and energy-recovery pumps. The membranes themselves reject dissolved salts, so clean permeate exits one side while concentrate carries the rejected ions to drain or recovery.
3. Post-Treatment and Remineralization
After the membranes, post-treatment tailors the water to its final use. In many plants, this means pH correction, remineralization for drinking water, or UV sterilization for microbial safety. When your process needs ultrapure water, we add an EDI (electrodeionization) polishing stage that reaches resistivity up to 18 MΩ·cm. Consequently, a single treatment train can serve both potable and ultrapure demands.
4. Controls, Monitoring, and Automation
Finally, instrumentation and a PLC turn a collection of components into a smart, self-protecting plant. Chunke integrates control platforms and instruments from Siemens, Schneider Electric, and Endress+Hauser so operators see conductivity, flow, pressure, and pump status in real time. Therefore, alarms trigger before small problems become expensive failures.
Industrial Reverse Osmosis System Flow Chart:
Industrial Reverse Osmosis System Capacities and Models
Chunke builds industrial reverse osmosis systems across a wide capacity band, so the same engineering discipline scales from a compact bottling line to a coastal desalination plant. The table below shows representative ranges. However, we size every unit to your exact flow, feed TDS, and recovery target rather than forcing your project into a fixed model.
| Capacity | System Type | Typical Feed Water | Common Applications |
|---|---|---|---|
| 100 – 2,000 LPH | Compact BWRO skid | Tap / brackish | Labs, small bottling, hotels |
| 2 – 10 m³/h | Single-pass industrial RO | Brackish / well | Food & beverage, textile |
| 10 – 50 m³/h | Single / double-pass RO | Brackish / municipal | Beverage, power, pharma pre-treatment |
| 50 – 300 m³/h | Large BWRO / containerized | Brackish / surface | Municipal supply, mining |
| Up to 7,500 m³/day | Seawater RO (SWRO) | Seawater (~35,000 ppm) | Desalination, islands, coastal industry |
For high-purity or high-rejection duties, a double-pass reverse osmosis system sends first-pass permeate through a second membrane bank. In contrast, when your site needs fast deployment, a containerized reverse osmosis system arrives pre-assembled and tested inside a shipping container. Both options use the same core platform, so you gain flexibility without sacrificing quality.
Key Components That Define System Quality
The gap between a professional industrial reverse osmosis system and a cheap copy lives inside the components. Two machines can look identical on the outside, yet perform very differently after a year of service. For that reason, Chunke specifies proven, brand-name parts and documents every one of them on your quotation.
Membranes
The membrane is where separation actually happens, so element quality drives both output and running cost. Chunke works with leading membrane brands including DuPont FilmTec, Toray, Hydranautics, and Vontron. Because these elements hold their rejection rate over time, your permeate quality stays predictable and your replacement intervals stretch out.
High-Pressure Pumps and Energy Recovery
Pumps set the energy bill, especially for seawater duty. Accordingly, we use efficient high-pressure pumps and, for SWRO, energy-recovery devices that cut specific energy consumption by half. Trusted pump and drive suppliers such as Grundfos and Danfoss keep the system efficient and serviceable worldwide.
Pressure Vessels and Piping
Membrane housings and piping must hold pressure safely for years. Therefore, Chunke uses certified ROPV membrane pressure vessels and industrial piping from suppliers such as Georg Fischer (+GF+). As a result, the high-pressure loop resists corrosion and fatigue in demanding coastal and industrial environments.
Instrumentation and PLC Control
Reliable measurement keeps the plant safe and efficient. Consequently, we fit conductivity, flow, and pressure instruments plus a PLC/HMI package so operators run the system with confidence. This automation also logs performance, which makes troubleshooting and warranty support far easier.
What is the price of industrial reverse osmosis machine?
An industrial reverse osmosis purification system cost is largely dependend on feed water quality and the required product water quality.
The following list details many of the common pre and post treatment components:
- Chemical and pH dosing for example SEKO
- Media filter for example quartz sand
- Carbon filter
- Water softener
- Antiscalant dosing
- Advanced controller
- Advanced instruments
- Iron removal filter for example greensand
- TDS, pH, Conductivity monitoring
- Stainless Steel Skid or frame
- Blending systems
- Three phase electrical system and accessories
- PLC components
- Touch Panel for example Siemens
- CIP membrane cleaning system
Water Sources and Industrial Applications
Feed water dictates the entire design, so Chunke matches the platform to your source before we quote a single component. Broadly, industrial reverse osmosis systems treat three water types, and each one calls for a different membrane, pressure, and recovery strategy.
Brackish Water RO (BWRO)
Brackish sources — wells, rivers, and municipal supply — usually carry under 10,000 ppm of dissolved salts. Because pressures stay moderate, a brackish water reverse osmosis system offers high recovery, often 65% to 80%, at lower energy cost. This makes BWRO the workhorse for bottling, food processing, textiles, and general industry.
Seawater RO (SWRO)
Seawater carries around 35,000 ppm of salt, so it demands high-pressure pumps, seawater-grade membranes, and energy recovery. Our seawater reverse osmosis systems turn ocean or coastal water into potable and process water for islands, resorts, and shoreline plants. For deeper technical detail on large desalination projects, our dedicated site swro-plant.com seawater desalination systems covers configurations and case studies.
Process, Boiler Feed, and Ultrapure Water
Many plants need water far purer than drinking standard. In power stations, pharmaceuticals, and electronics, RO paired with EDI delivers ultrapure water for boilers and precision processes. Meanwhile, industries that reuse wastewater rely on RO to recover valuable water and meet discharge limits. Across all of these, one principle holds: the cleaner and more stable the feed, the longer your membranes last — which is why our engineers always start with your water report.
To picture where these plants add value, consider the industries we supply every day. Bottled-water and beverage producers depend on RO for consistent taste and product safety. Power stations and boiler houses need low-conductivity make-up water to prevent scale and corrosion. Pharmaceutical and electronics factories demand ultrapure grades, whereas mines, hotels, and municipalities use RO to secure a dependable supply from difficult sources. In each case, the same disciplined engineering keeps output steady and running costs predictable.
What is the electrical power consumption of RO System?
It depends on capacity of ro water purifier plant as liter per hour or liter per day. So, our ro water treatment system power supply range is 220V to 480V with 50Hz or 60Hz.
In the realm of industrial water treatment, Reverse Osmosis (RO) systems have emerged as a leading technology to purify water, ensuring high-quality output while maximizing efficiency. RO systems have proven indispensable in various sectors, including manufacturing, power generation, pharmaceuticals, and food and beverage production. This essay delves into the world of industrial RO systems, exploring their significance, working principles, benefits, and key considerations for effective implementation.
Understanding Industrial Reverse Osmosis Systems
Industrial RO systems employ a process called reverse osmosis to purify water by removing impurities, contaminants, and dissolved solids. This technology utilizes a semi-permeable membrane that allows water molecules to pass through while rejecting dissolved solids, salts, and other unwanted particles. By exerting pressure on the feedwater, RO systems drive the water molecules against the concentration gradient, resulting in the separation of impurities and pure water.
Working Principles of Industrial RO Systems
An industrial RO system comprises several key components that work together to deliver clean water. Firstly, the pre-treatment stage involves the removal of larger particles, sediments, and organic matter through processes like filtration, sedimentation, and activated carbon adsorption. This helps protect the RO membrane from fouling and damage.
Next, the pressurization stage forces the pre-treated water into the RO membrane using a high-pressure pump. The semi-permeable membrane acts as a barrier, allowing only pure water molecules to pass through, while rejecting dissolved solids and contaminants.
The purified water, known as permeate, is collected and stored for use, while the concentrated wastewater, known as brine or reject water, is discharged from the system. Some advanced RO systems incorporate energy recovery devices to optimize efficiency by reusing the energy contained in the brine stream.
Buyers always ask about the price of an industrial reverse osmosis machine, and the honest answer is that it depends on your specification. Several factors move the number, so a like-for-like quote matters far more than a headline figure. Below are the main cost drivers.
First, capacity and feed water set the base cost, because seawater and high-recovery designs need more pumping power and membranes. Second, the level of automation, the frame material, and the brand of pumps and membranes shift the price. Third, options such as containerization, double-pass polishing, and EDI add capability and cost.
Beyond the purchase price, smart buyers weigh the total cost of ownership. A cheap system with weak membranes and an inefficient pump often costs more within two years through energy and replacements. In contrast, a professionally engineered Chunke system lowers your lifetime cost per litre. That is exactly why we position ourselves as a system-driven manufacturer rather than the cheapest box on the market. To compare configurations and specifications side by side, download our water treatment systems catalogue.
Benefits of Industrial RO Systems
High Water Quality: Industrial RO systems effectively remove a wide range of impurities, including heavy metals, salts, bacteria, and organic compounds. This ensures that the treated water meets stringent quality standards and is suitable for various industrial processes, ultimately enhancing product quality and safety.
Water Efficiency: RO systems have a high water recovery rate, typically ranging from 50% to 80%. This means that a significant portion of the feedwater can be converted into permeate, minimizing water wastage and reducing the overall water footprint of industrial operations.
Cost Savings: Implementing RO systems can lead to substantial cost savings in the long run. By producing purified water on-site, industries can avoid the expenses associated with purchasing and transporting large volumes of water. Additionally, the removal of contaminants and dissolved solids can prevent scaling and corrosion issues, reducing maintenance and equipment replacement costs.
Environmental Sustainability: Industrial RO systems contribute to environmental sustainability by conserving water resources and reducing the discharge of pollutants into ecosystems. By adopting RO technology, industries can align with sustainable practices and meet regulatory requirements, fostering a positive reputation and responsible corporate image.
Considerations for Effective Implementation
To ensure optimal performance and longevity of industrial RO systems, several considerations should be taken into account:
System Design: Proper system design, including accurate sizing, selection of appropriate membranes, and consideration of operational conditions, is crucial to achieving desired outcomes. Engaging with experienced professionals and reputable manufacturers is recommended to ensure an efficient and reliable system design.
Pretreatment: Effective pretreatment is essential to protect the RO membrane from fouling, scaling, and premature deterioration. Adequate prefiltration, pH adjustment, and chemical dosing systems tailored to the feedwater characteristics are necessary to optimize system performance.
Monitoring and Maintenance: Regular monitoring of system parameters, including pressure, flow rates, and water quality, is vital for detecting any deviations or issues
How to Choose the Right Industrial Reverse Osmosis System
Choosing an industrial reverse osmosis system is an engineering decision, not a shopping decision. Get the specification right, and the plant runs efficiently for a decade. Get it wrong, and you pay through fouled membranes, high energy bills, and downtime. Use the criteria below as your checklist.
Feed water analysis. Always start with a full analysis: TDS, hardness, silica, iron, SDI, and temperature. Because these values drive membrane choice and recovery, no honest supplier can size a system without them.
Capacity and recovery. Define your daily permeate demand and your recovery target. In turn, these numbers set the number of membranes, vessels, and the concentrate management approach.
Energy efficiency. For seawater and large plants, energy is the biggest lifetime cost. Therefore, insist on efficient pumps and energy recovery to protect your operating budget.
Automation and after-sales. A PLC-controlled system with remote monitoring lowers labour and protects the membranes. Just as important, confirm the supplier can deliver spare parts and support in your region. Chunke ships spares and technical guidance to customers worldwide, which keeps your plant productive long after commissioning.
Footprint and installation. Site space, ceiling height, and ambient temperature all shape the layout. For tight or remote locations, a containerized build removes civil work and shortens commissioning. Plan access for membrane changes and CIP connections from the start, because good layout saves hours on every service visit.
Membrane cleaning. Every RO plant fouls over time, so plan for it. A dedicated CIP membrane cleaning system restores flux and extends membrane life, which directly lowers your cost per cubic metre.